

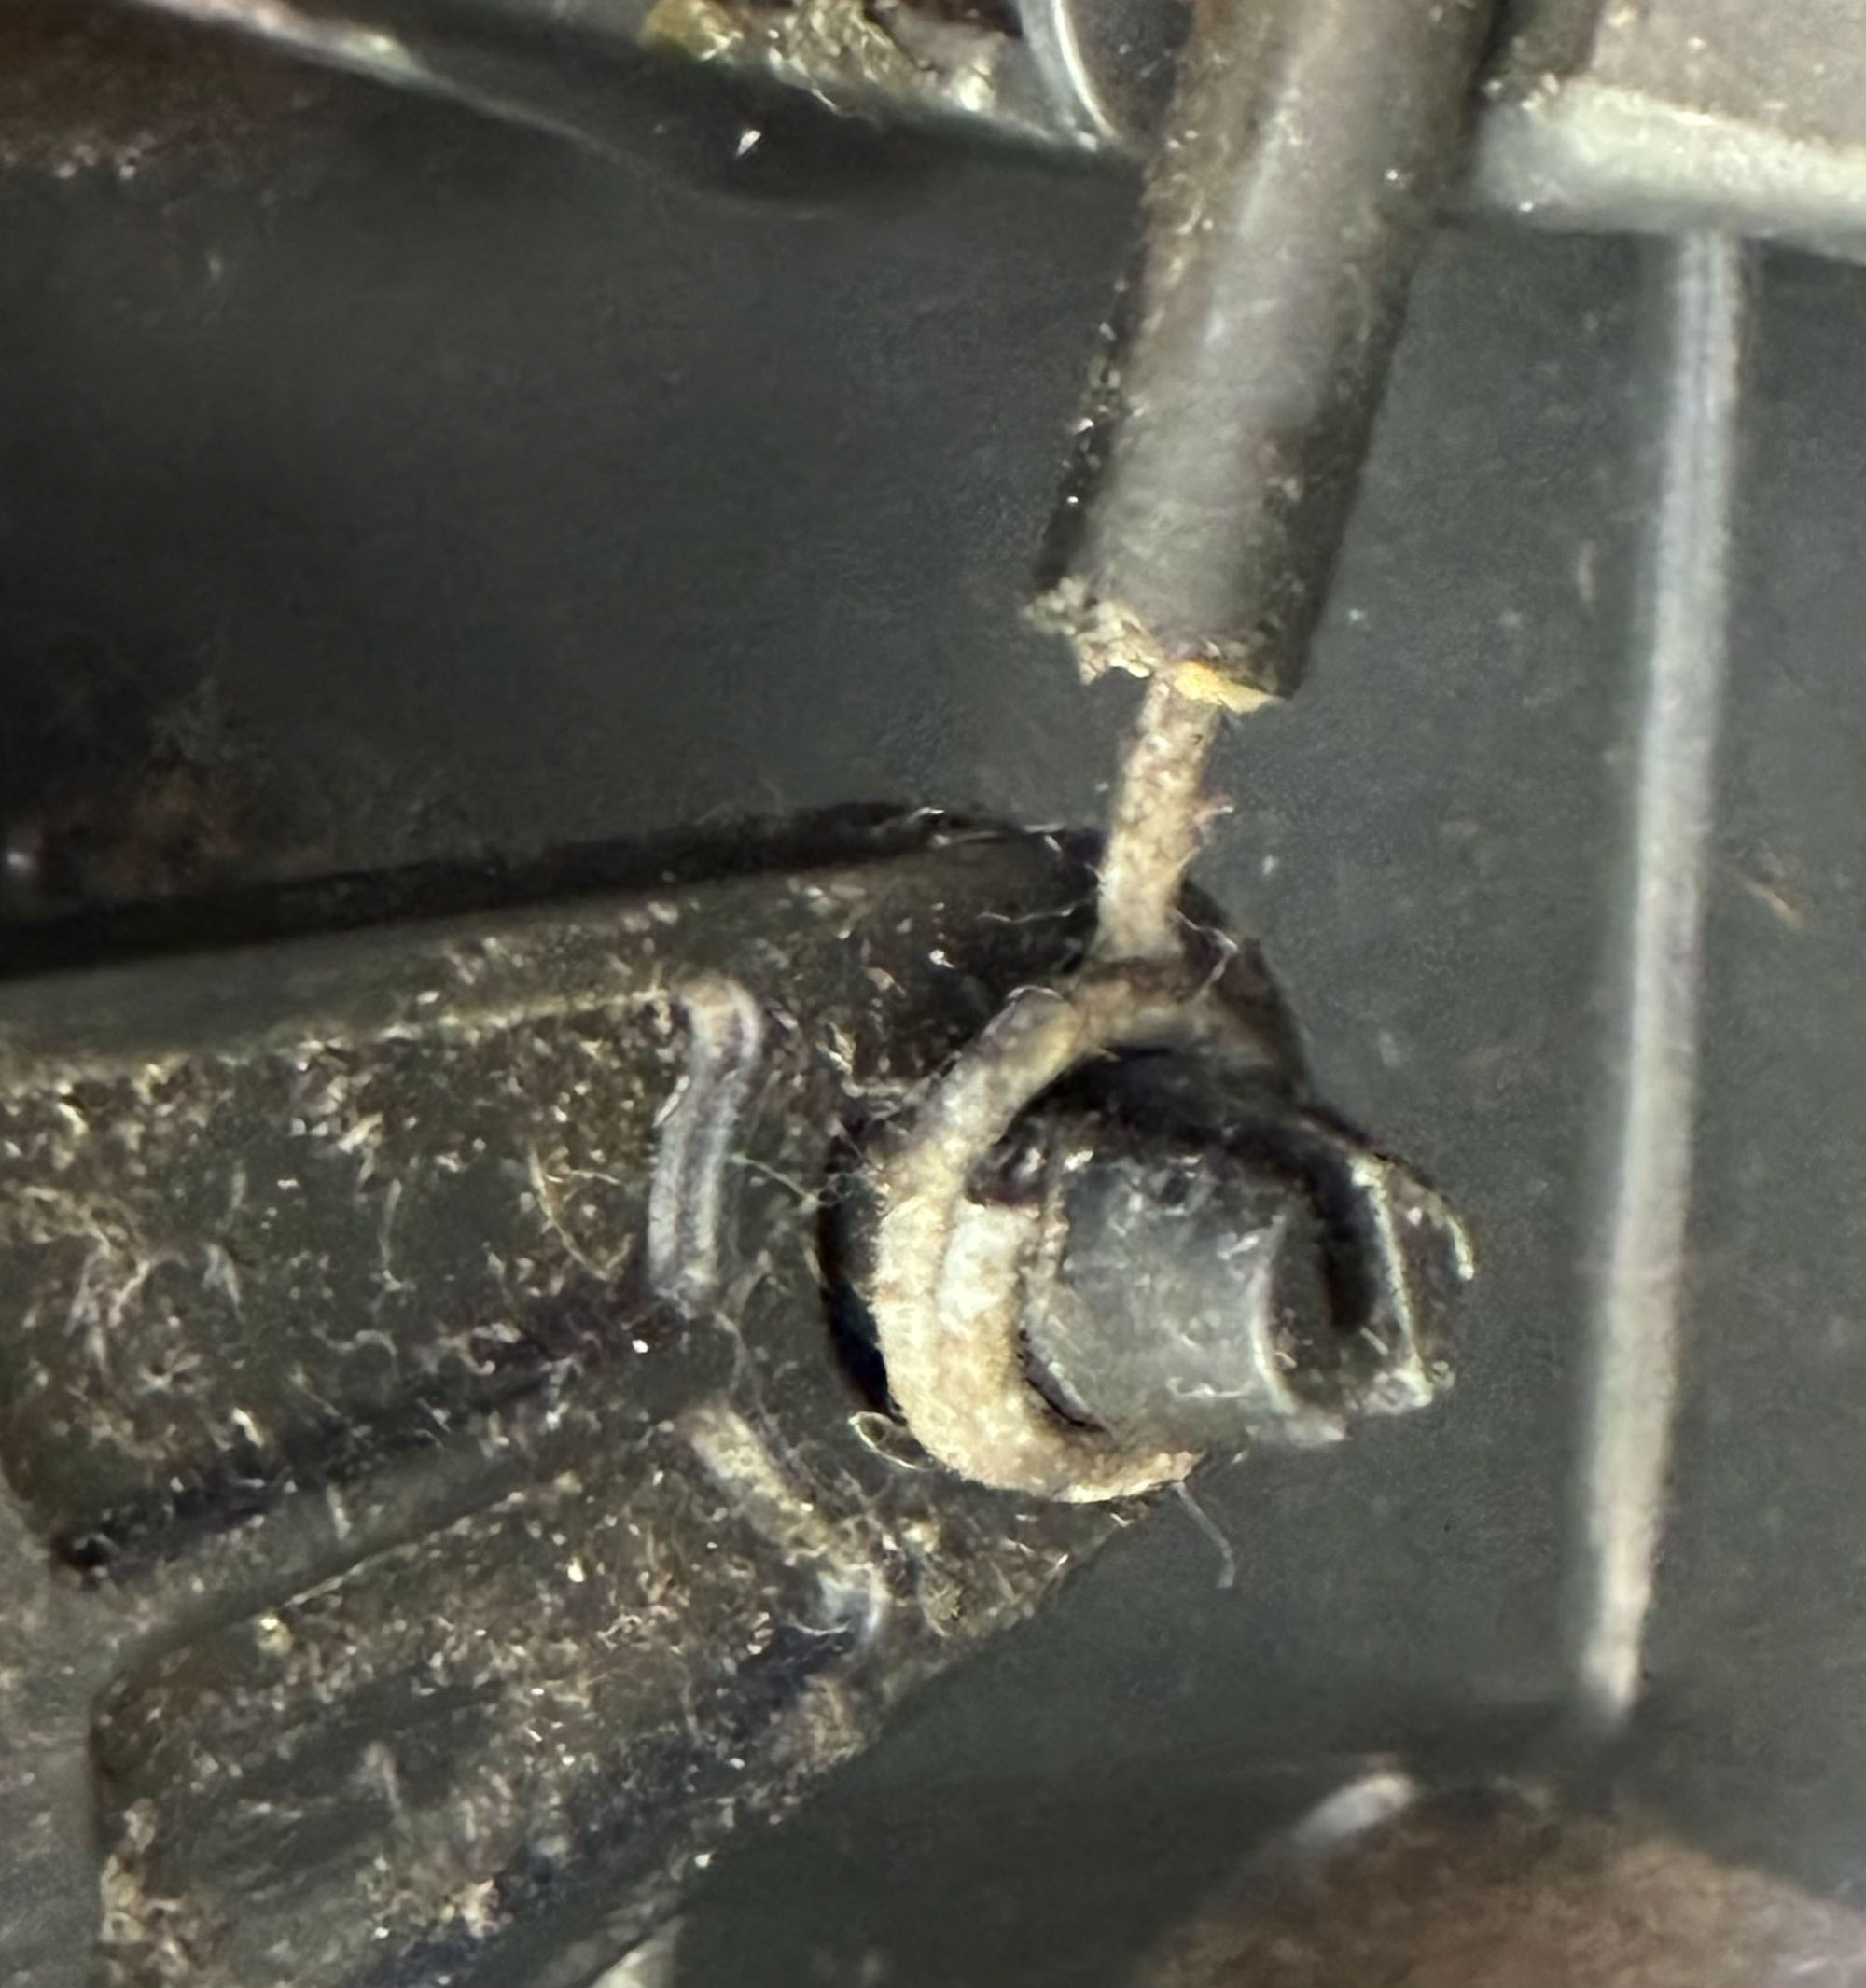
The previous two parts of this series gave an introduction to control cables, discussed options when buying, and analyzed different methods of attaching control cables to your aircraft. In my own build experience with two different airplanes, I was left wanting more: better attachment methods, the ability to terminate in my own shop, less friction, and so on. I decided there must be a better way and settled on a third option: the coiled, or rolled, wire end. It allows for a properly torqued, bolted joint and very low-friction swivel action. It also does not require crushing or damaging the inner wire each time the cable is attached and removed.
Car manufacturers have been using this style for decades to terminate push-pull cables, and I have seen several examples of Jabiru engine installations with rolled cable ends done by professional shops. As mentioned in Part 2, there is not really a list of approved methods for this sort of thing. Testing and legacy seem to be the most important factors to call something “approved.” Heck, rumor has it that Jim Bede certified the Grumman American AA-1 Yankee with a Sears lawnmower choke cable installed for the mixture control.
The only trouble is how to make a nice rolled end. I searched extensively and could only find a couple examples of homemade tools to do the job, so I designed my own. It is a pretty simple tool to use, especially after a practice round on some extra wire.
There are 12 steps to follow:
- Route the cable in the installed configuration.
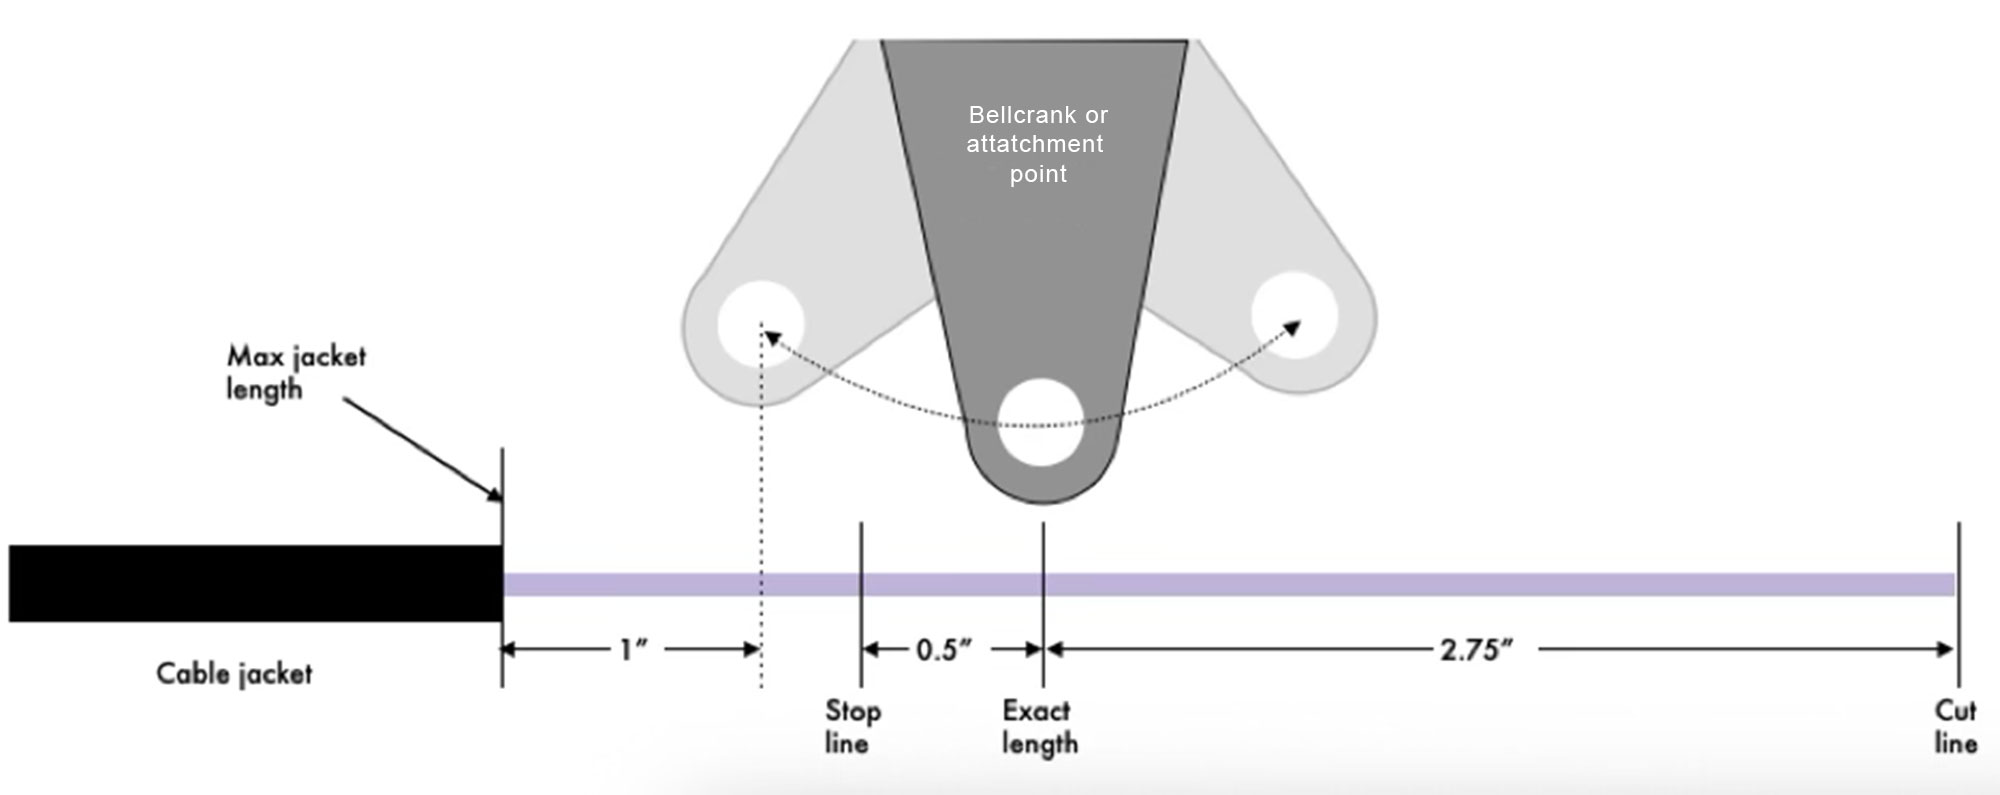
- Cut the outer cable jacket back to allow full stroke of the attachment point. Leave inner wire long.
- Mark the exact length of termination on the inner wire at the bellcrank or attach point. Make sure to set your control knob and bellcrank at comparable positions; mid-stroke is a good choice.
- Mark two offset locations: one “stop line” shorter than the first mark by half-inch, and one “cut line” longer by 2.75 inches.
- Cut the inner wire on the cut line.
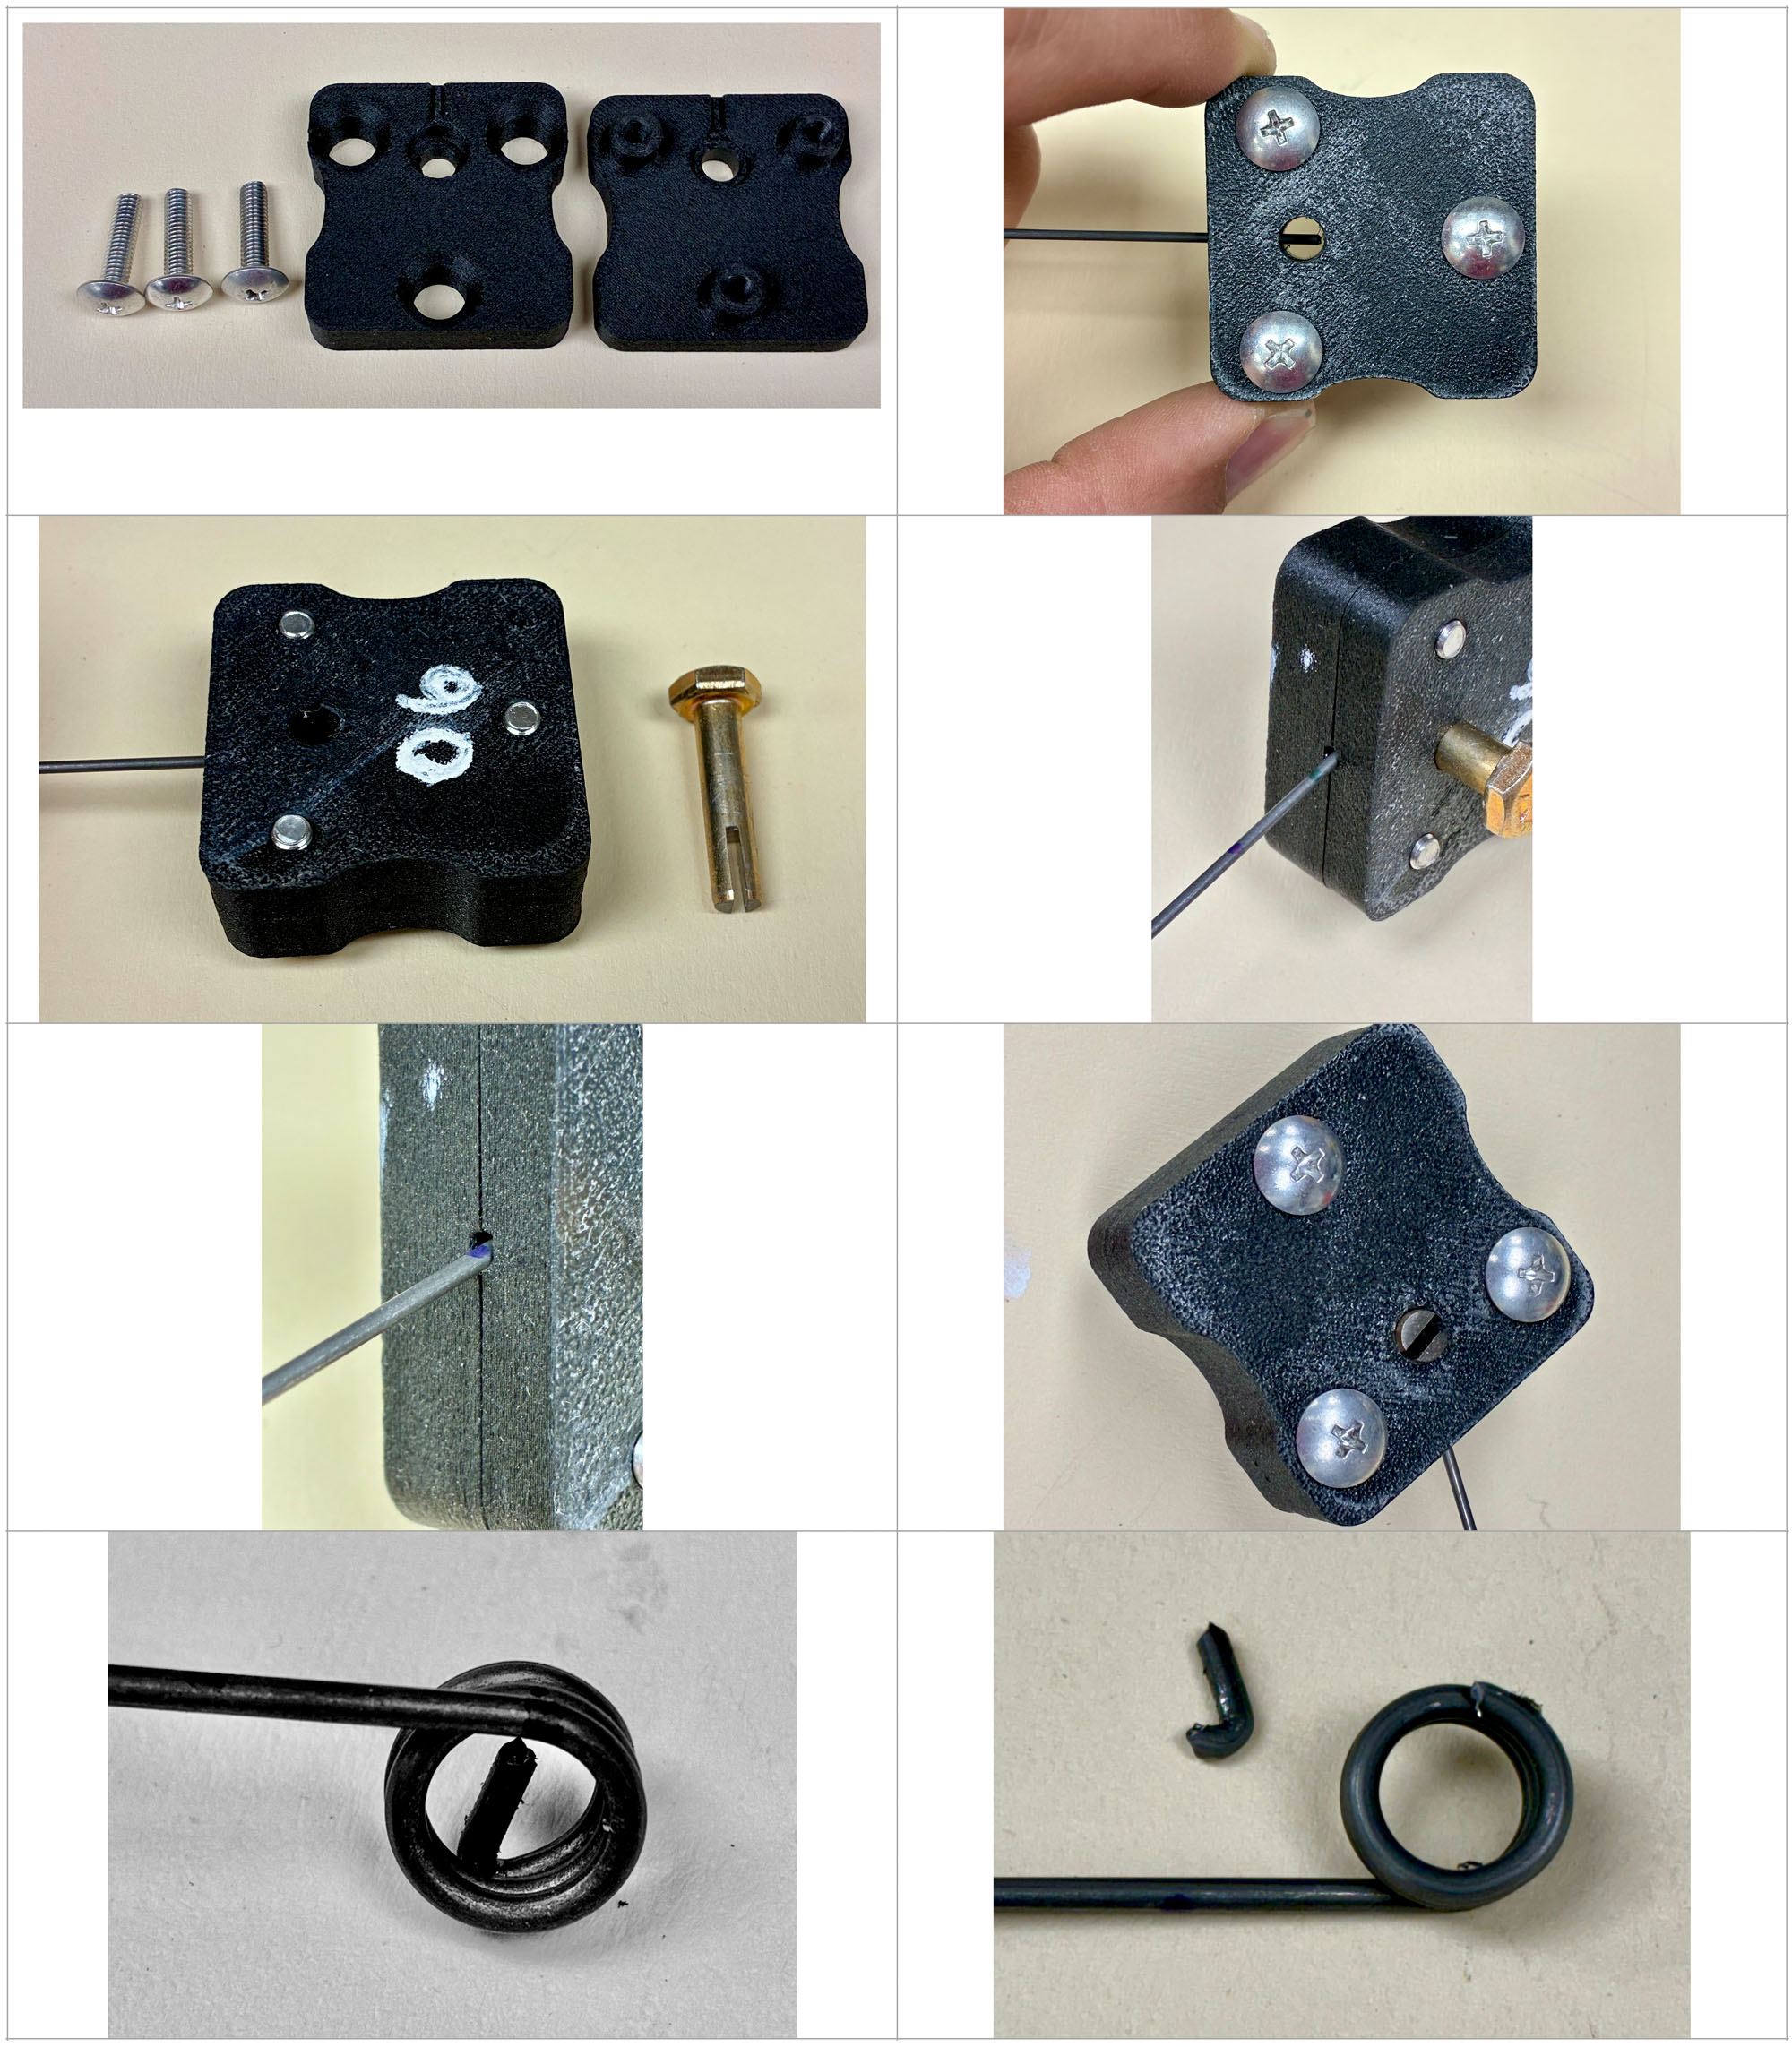
- Insert the wire into the tool and clamp with three screws.
- Insert the slotted “crank” fastener and engage the wire fully in the slot.
- Rotate the crank three-quarter turns without pushing it down at all.
- Continue to rotate the crank while gently pushing down to create the spiral wrap of the coil.
- Stop cranking when you see the “stop line” at the edge of the tool.
- Open up the tool and remove the coiled end.
- Trim the tail that crosses through the center and deburr.
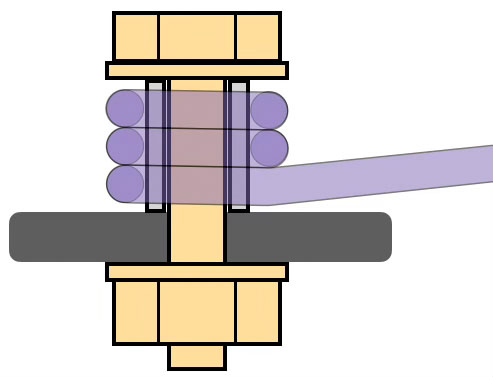
This process leaves you with three coils of wire, which seems to work great and provide adequate grip length for the appropriate AN3 bolt. I use a sleeve bushing with 3/16-inch ID and 1/4-inch OD that is cut just slightly longer than the coil width. Next, an AN3 bolt can be tightened across the bushing and bellcrank without binding the cable wire. Then you are done!

I have done some pull-testing on this type of attachment to address the concern of the coil “unraveling” under tension. I never had this concern working with the wire since it is so difficult to coil in the first place (see Part 2, “Strength”). Nonetheless, I tested the force required to unravel several coiled ends, and it came out to around 150 pounds. By my estimates, this is in the ballpark of a 15- to 20-time margin on what we apply to control cables with our hands. A 150-pound pull force might even rip the panel out of some airplanes. These results should be treated as a loose reference since cable inner wires can vary in material and diameter from around 0.055 to 0.070 inch. I measured several bellcranks on my aircraft that required only a few ounces of force to actuate. Note that any friction forces due to the cable routing are not felt by the end attachment.
There are some other interesting features of this design to point out. Unlike a tensile failure or set screw slippage, control would not be lost until the entire coil unravels. Incipient failure as shown here could be detected via visual inspection and will also point to a sudden increase in friction or a likely issue on the related bellcrank.
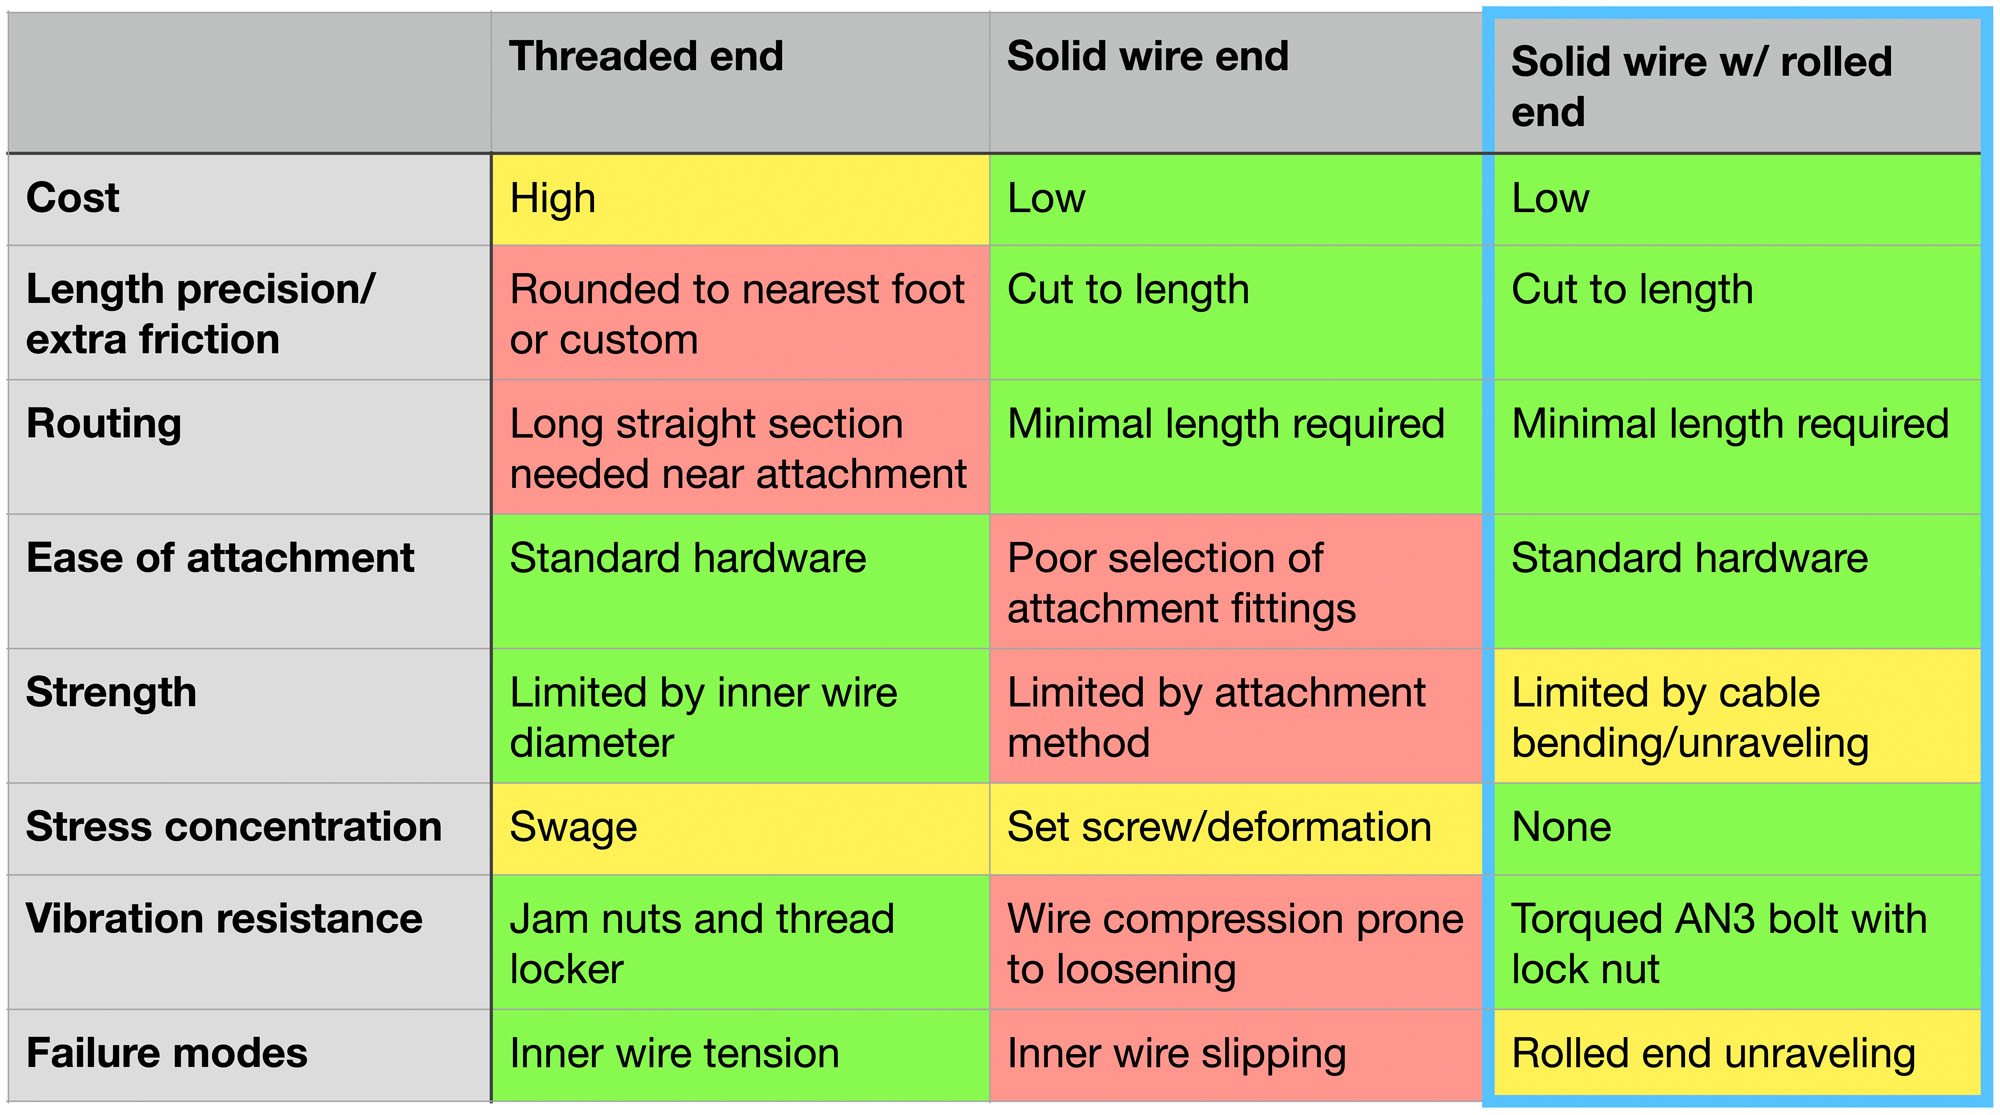
The rolled end solves pretty much all the issues that we pointed out in Part 2 of this series. Since we are still starting with a solid wire end control, we keep the benefits of cost and length precision. Now the attachment method has been improved so it no longer complicates assembly and disassembly by damaging the solid wire. The failure mode now sits between our previous two options with the unraveling phenomenon. It is slightly weaker than pure tension, but it is much more predictable and secure than a set-screw-style attachment.
The most important gain from this style of attachment is eliminating stress concentrations. The coiled end has no diameter reduction or stresses applied to the surface. The gradual curve of the inner wire into a cylindrical coil is about the most gentle treatment we can give it from an engineering standpoint. In fact, the way in which it fails is indicative of the lack of stress concentrations.
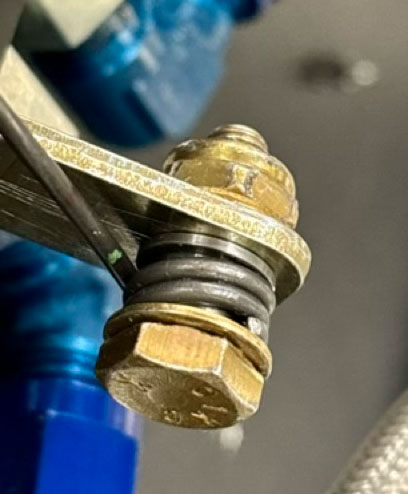
There are a couple new factors to consider with the rolled end if you are accustomed to solid wire controls the old-fashioned way. One is that you can no longer remove the inner wire for cleaning or servicing. The second is that the end of the cable now has a fitting that is about 3/8-inch diameter, which is larger than the cable jacket diameter. So make sure your firewall penetration has at least a 3/8-inch-diameter opening. Eyeball fittings and most collet-type clamps can accommodate this.
After seeing the results firsthand, using the tools, and testing the finished cables, I felt inspired to share this capability with others. There is something incredibly satisfying about starting with the most basic form that is Bowden cable and terminating it to the perfect length with basic tools. The end result is incredibly low friction, lightweight, robust, and vibration resistant.
I set up some small-batch manufacturing capability and offer the tool for sale. Please reach out if you would like one for yourself: taz@zelwing.net. Then you can customize your own cables and get the perfect length every time!

I enjoyed this article and the author did a great job of describing various options, testing he did, and and describing the tooling he built.
How about a dimensioned drawing for the tool? What is is made of?
Hello, while I don’t have a drawing for you, I can share some details on the material. It is 3D printed using a high strength carbon fiber reinforced nylon. The “crank” is a machined bolt and the clamp screws are steel 10-32. I originally tried it with a cheap PLA print, and though it worked, it wouldn’t last much longer than a couple operations. The nylon is much more robust. Thank you for the comment.
Good article, Troy. I have limited experience on control cables, but I like the concept. How easy is it to coil the inner conductor? I thought these were spring steel and would be difficult to form so that they maintained the coil O.D.?
Hi Mike, your are correct that the inner wire is very stiff and difficult to coil. This led me to make the tool which preserves the correct shape. Doing it with pliers or an open form would be very difficult!
Got it. Thanks Troy. I was thinking more about this… The only places I have control cables are for my Rotax 912ULS (uses setscrews and a sliding “safety ferrule”, also with setscrews.) I need to get to the plane and look at that again.